Choosing an Electric Vehicle Mold is not merely a purchasing decision. It affects battery safety, panel accuracy, production speed, and long-term maintenance costs.
A reliable mold must match the resin, part geometry, expected volume, and factory equipment. Battery housings often demand stable dimensions, controlled warpage, and carefully balanced cooling channels. Exterior panels may require excellent surface finish, uniform wall thickness, and minimal weld lines. Small design mistakes can appear as sink marks, flash, uneven texture, or difficult ejection. They may only become visible after thousands of cycles.
Dr. W. Edwards Deming, a respected manufacturing quality authority, said, “Quality comes not from inspection, but from the improvement of the production process.” That principle applies strongly to Electric Vehicle Mold selection. A supplier should explain steel grade, mold-flow analysis, cooling performance, tolerance control, trial-shot results, and maintenance planning. Ask for measurable evidence, not polished promises. Check cycle time under realistic conditions. Review previous projects with similar materials and shapes. Confirm spare-part availability and technical response time. Consider automation compatibility, energy use, and future design changes.
No checklist is perfect. I have seen attractive quotations hide weak cooling layouts and unclear acceptance standards. That experience makes one point difficult to ignore: the cheapest mold may become the most expensive asset. The following ten tips help buyers compare suppliers more carefully, identify technical risks earlier, and choose a mold that performs consistently on the production floor.
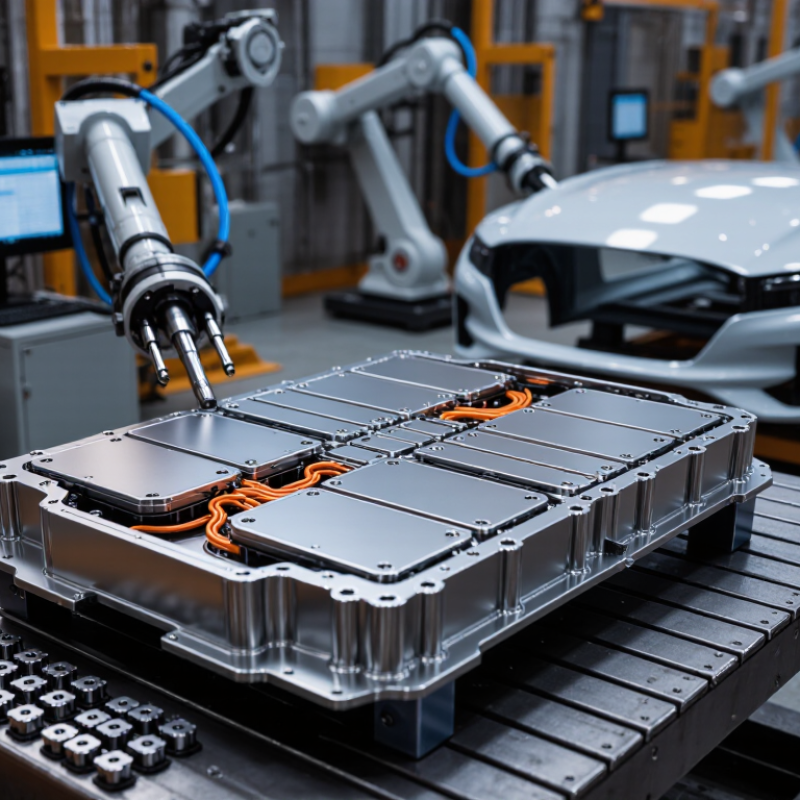
Choosing an electric vehicle mold begins with a clear definition of its purpose. Is it designed for a battery housing, dashboard panel, charging connector, or structural component? Each part demands different mold geometry, material compatibility, and cooling performance. A battery cover may need tight sealing surfaces, while an interior panel may prioritize texture and appearance. Confusing these goals can create expensive redesigns.
Production requirements should be written before discussing mold construction. Record the selected plastic, expected annual volume, part dimensions, wall thickness, tolerance range, and target cycle time. For example, a 2.5-millimeter wall may require balanced cooling to prevent warpage. Large parts also need careful ejection planning. Check whether the mold will run in a single-cavity trial or a high-volume multi-cavity system. Small details matter.
Ask for evidence from previous projects, such as measured cycle times, dimensional inspection records, and mold maintenance histories. Reliable engineering decisions should come from data, not attractive promises. Confirm the machine’s clamping force, injection capacity, and available mold space. These limits are often overlooked. A mold may look suitable on paper but fail during installation. Review venting, cooling channels, steel selection, and replacement components with experienced technicians. Build in inspection points for flash, sink marks, weld lines, and uneven shrinkage. A perfect first estimate is rare. Leave room to learn from the first trial.
Define the Electric Vehicle Mold’s Purpose and Production Requirements
Representative engineering values for common injection-molded electric vehicle components. Battery trays and covers generally require thicker sections and longer cooling cycles, while connector housings require tighter dimensional control and thinner walls. Actual mold specifications should be validated against the selected polymer, part geometry, annual volume, tolerances, and production equipment.
Tip 1: Match the mold material to the production load.
Aluminum molds suit prototypes and short runs because they machine quickly and cost less. However, they can wear faster under glass-filled engineering plastics. Pre-hardened tool steel offers better durability for medium-volume electric vehicle parts. Hardened steel usually performs better for demanding battery housings and structural components.
Tip 2: Examine abrasion, heat, and corrosion risks together.
Reinforced polymers can polish or erode cavity surfaces over time. Repeated heating and cooling may also create small cracks near sharp corners. In practical mold inspections, these details often matter more than the original material price. Ask for hardness data, impact resistance, and documented maintenance records.
Tip 3: Estimate service life from cycles, not vague promises.
A reliable supplier should connect expected cycles with material grade, part geometry, cooling design, and repair history. Proper venting and balanced cooling can protect the mold from unnecessary stress. Still, service life is never perfectly predictable. I have seen well-built molds decline early because cleaning was inconsistent. That uncomfortable detail deserves attention.
Check replaceable inserts, wear plates, and surface treatments before approval. These features can reduce repair time and extend useful production life. Also inspect the mold after trial runs. Tiny flashes, uneven texture, or rising injection pressure may signal early wear. A lower purchase price can become expensive when downtime begins.
10 Tips to Choose the Best Electric Vehicle Mold
When choosing an electric vehicle mold, precision should guide every technical discussion. Check cavity tolerances, parting-line alignment, and insert repeatability before reviewing the quotation. A few microns can affect battery housings, sensor brackets, and connector covers. Ask how measurements are verified. Coordinate measuring machines, inspection reports, and trial records provide stronger evidence than confident promises.
Surface quality also deserves close attention. Inspect sample parts under angled light, not only in standard factory lighting. Look for flow marks, weld lines, sink marks, and uneven texture around ribs. A smooth cavity does not always create a flawless surface. Resin behavior, cooling balance, and gate placement matter too. I once trusted a polished mold face and overlooked poor cooling. The result looked acceptable, but warped after production.
Design compatibility connects these details. Review draft angles, wall thickness, undercuts, ejector locations, and expected material shrinkage with the mold engineer. The mold must suit both the component geometry and its production process. Ask whether cooling channels can reach thick sections without weakening the tool. Request a mold-flow study when the part has long flow paths or tight cosmetic requirements. Keep decisions documented. Small changes often become expensive later. A design can be technically possible yet difficult to maintain. That distinction is easy to miss.
| No. | Evaluation Dimension | Recommended Selection Benchmark | Verification Method | Suggested Weight | Why It Matters for EV Parts |
|---|---|---|---|---|---|
| 1 | Dimensional Precision | Set tolerances according to the part function. A general molded-part target is commonly around ±0.10–0.20 mm, while critical interfaces may require tighter control. | Review the GD&T drawing, CMM reports, capability studies, and first-article inspection results. | 18% | Accurate dimensions support reliable assembly of battery housings, sensor mounts, connectors, and interior modules. |
| 2 | Surface Quality | Define an approved surface standard, such as a controlled texture, uniform gloss, and no visible sink marks, weld lines, scratches, or flow defects in Class-A areas. | Use visual inspection under consistent lighting, gloss measurement, surface comparators, and approved master samples. | 14% | Visible EV interior and exterior components strongly influence perceived quality and customer acceptance. |
| 3 | Design Compatibility | Confirm compatibility with wall thickness, draft angles, ribs, bosses, clips, undercuts, inserts, and required ejection locations before mold construction. | Conduct DFM and mold-flow reviews using the latest 3D CAD data and revision-controlled drawings. | 14% | Proper design integration reduces rework, warpage, short shots, and assembly interference. |
| 4 | Material and Steel Selection | Choose mold materials according to resin abrasiveness, glass-fiber content, corrosion risk, production volume, and required surface finish. | Check material certificates, hardness records, heat-treatment documentation, and corrosion-protection specifications. | 10% | Appropriate steel and treatment improve wear resistance, dimensional stability, and mold service life. |
| 5 | Cooling Efficiency | Require balanced cooling coverage, adequate channel spacing, and temperature uniformity suited to the part geometry and resin. | Review cooling simulations, circuit layouts, temperature measurements, and cycle-time trial data. | 10% | Consistent cooling helps control cycle time, shrinkage, warpage, and dimensional variation. |
| 6 | Mold-Flow and Warpage Control | Evaluate filling balance, pressure, weld-line position, air traps, fiber orientation, shrinkage, and predicted deformation before machining. | Request a mold-flow report and compare predicted results with trial-part measurements. | 10% | Large thin-wall EV panels and structural plastic parts are particularly sensitive to filling and warpage behavior. |
| 7 | Gating and Ejection Design | Select gate locations that minimize cosmetic defects and residual stress; ensure ejector pins, sleeves, lifters, and slides do not mark functional surfaces. | Review the mold layout, gate study, ejection-force analysis, and trial-part appearance. | 8% | Correct gating and ejection improve part release, cosmetic quality, and dimensional repeatability. |
| 8 | Cycle-Time and Automation Readiness | Assess hot-runner suitability, part handling, robot access, mold-open sequence, cycle-time target, and compatibility with the intended molding machine. | Verify machine calculations, automation interface drawings, and production-trial cycle records. | 7% | Efficient and repeatable production lowers unit cost and supports high-volume EV manufacturing. |
| 9 | Maintenance and Replaceability | Use accessible wear components, standardized spare parts, clear lubrication points, replaceable inserts, and documented preventive-maintenance intervals. | Inspect maintenance manuals, spare-part lists, component drawings, and service-access features. | 5% | Fast maintenance minimizes unplanned downtime and protects production continuity. |
| 10 | Validation and Documentation | Require a complete validation package covering dimensional inspection, material traceability, process parameters, trial records, changes, and acceptance criteria. | Audit the inspection plan, control plan, qualification records, revision history, and final acceptance report. | 4% | Traceable documentation supports quality audits, engineering changes, and stable long-term production. |
| Total Evaluation Weight | 100% | Use the weighted score to compare shortlisted mold proposals objectively. | |||
Electric vehicle molds often face tight tolerances, large surfaces, and demanding production cycles. Cost should include steel, machining, trials, repairs, and rejected parts. A low quotation may hide expensive design changes. Request a detailed cost breakdown before approval. The mold structure should match the expected volume. For a prototype, modular inserts can reduce early spending. For mass production, hardened steel may justify its higher price. The IEA’s Global EV Outlook 2024 reports nearly 14 million electric cars were sold globally in 2023. That growth increases pressure on stable, repeatable tooling.
Maintenance affects delivery more than many buyers expect. Ask about cooling-channel access, replaceable inserts, lubrication points, and spare components. A clogged channel can create uneven shrinkage across a large door panel. The U.S. Department of Energy notes that electric vehicles generally need less vehicle maintenance because they contain fewer moving parts. The mold is different. It still needs disciplined cleaning and inspection. I usually require a maintenance checklist after every production run, although this step is sometimes ignored under schedule pressure.
Delivery time should include design review, steel preparation, machining, assembly, sampling, and correction rounds. Eight to twelve weeks may be realistic for a standard mold, but complex battery-tray tooling can take longer. Confirm the trial-shot quantity and acceptance criteria in writing. Also ask for measurable mold-flow results. Small changes matter. A missed cooling detail can delay shipment more than an expensive material choice. The U.S. National Institute of Standards and Technology emphasizes measurement traceability; suppliers should provide inspection records, not only promises.
Choosing an electric vehicle mold begins with the supplier, not the quotation. Ask for evidence of experience with battery housings, interior modules, or charging components. Request sample inspection reports, mold-flow studies, and references from comparable production volumes. A polished presentation is not proof.
During a factory visit, examine machining records, trial-mold notes, and how technicians measure steel temperature. These details reveal practical knowledge. I have learned that suppliers often describe “tight tolerance” without defining the actual range.
Quality standards must be specific to the mold and its use. Check whether the supplier operates under ISO 9001 and applies IATF 16949 practices where appropriate. Verify calibration certificates for CMMs, gauges, and temperature sensors.
Review steel certificates, heat-treatment records, cavity balance data, and first-article results. Ask how they control flash, sink marks, weld lines, and warpage. Standards help, but paperwork can hide weak process control. That is an uncomfortable point.
Technical support should continue after shipment. Confirm response times, spare-part planning, remote troubleshooting, and on-site trial support. Ask who owns design changes when cooling performance misses the target. A clear escalation path prevents costly production pauses.
Require 2D drawings, 3D files, maintenance schedules, and documented acceptance criteria. Test their support before signing: send a realistic mold problem and assess the technical reply. One vague answer matters. Good suppliers explain limitations, suggest measurable corrections, and record lessons from every trial. Even experienced teams make mistakes; transparent correction is more reliable than confident promises.